Explore our premium selection of industrial-grade server components, high-speed memory modules, and specialized hardware designed for mission-critical enterprise applications.
Backed by rigorous operational metrics, robust supply chain networks, and an unwavering commitment to excellence in global electronics manufacturing.
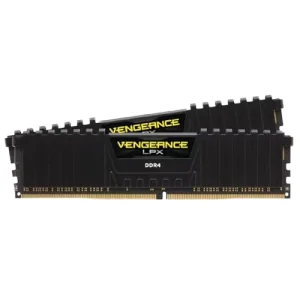
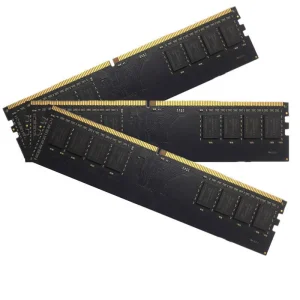
CoreByte Storage Technology Co., Ltd. is a professional DDR5 memory and DRAM solution manufacturer specializing in high-performance memory modules for global OEM, enterprise, and data center applications. Established in 2016, the company has developed strong capabilities in R&D, production, and international trade, focusing on stable, high-speed, and energy-efficient memory products.
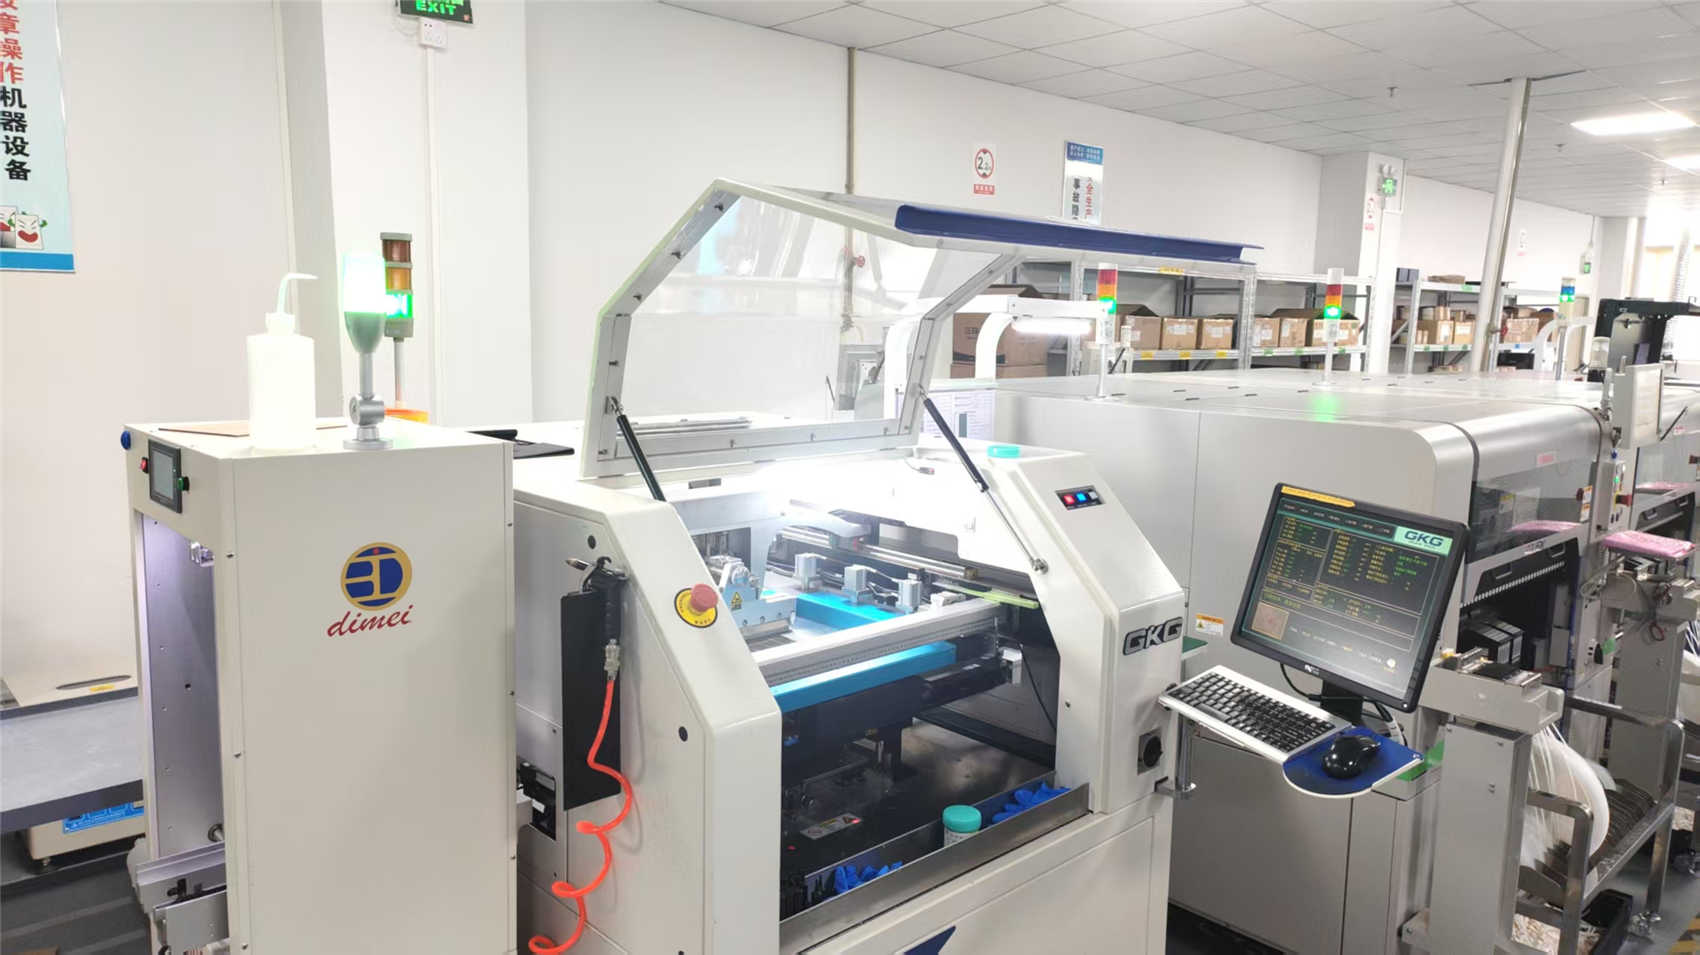
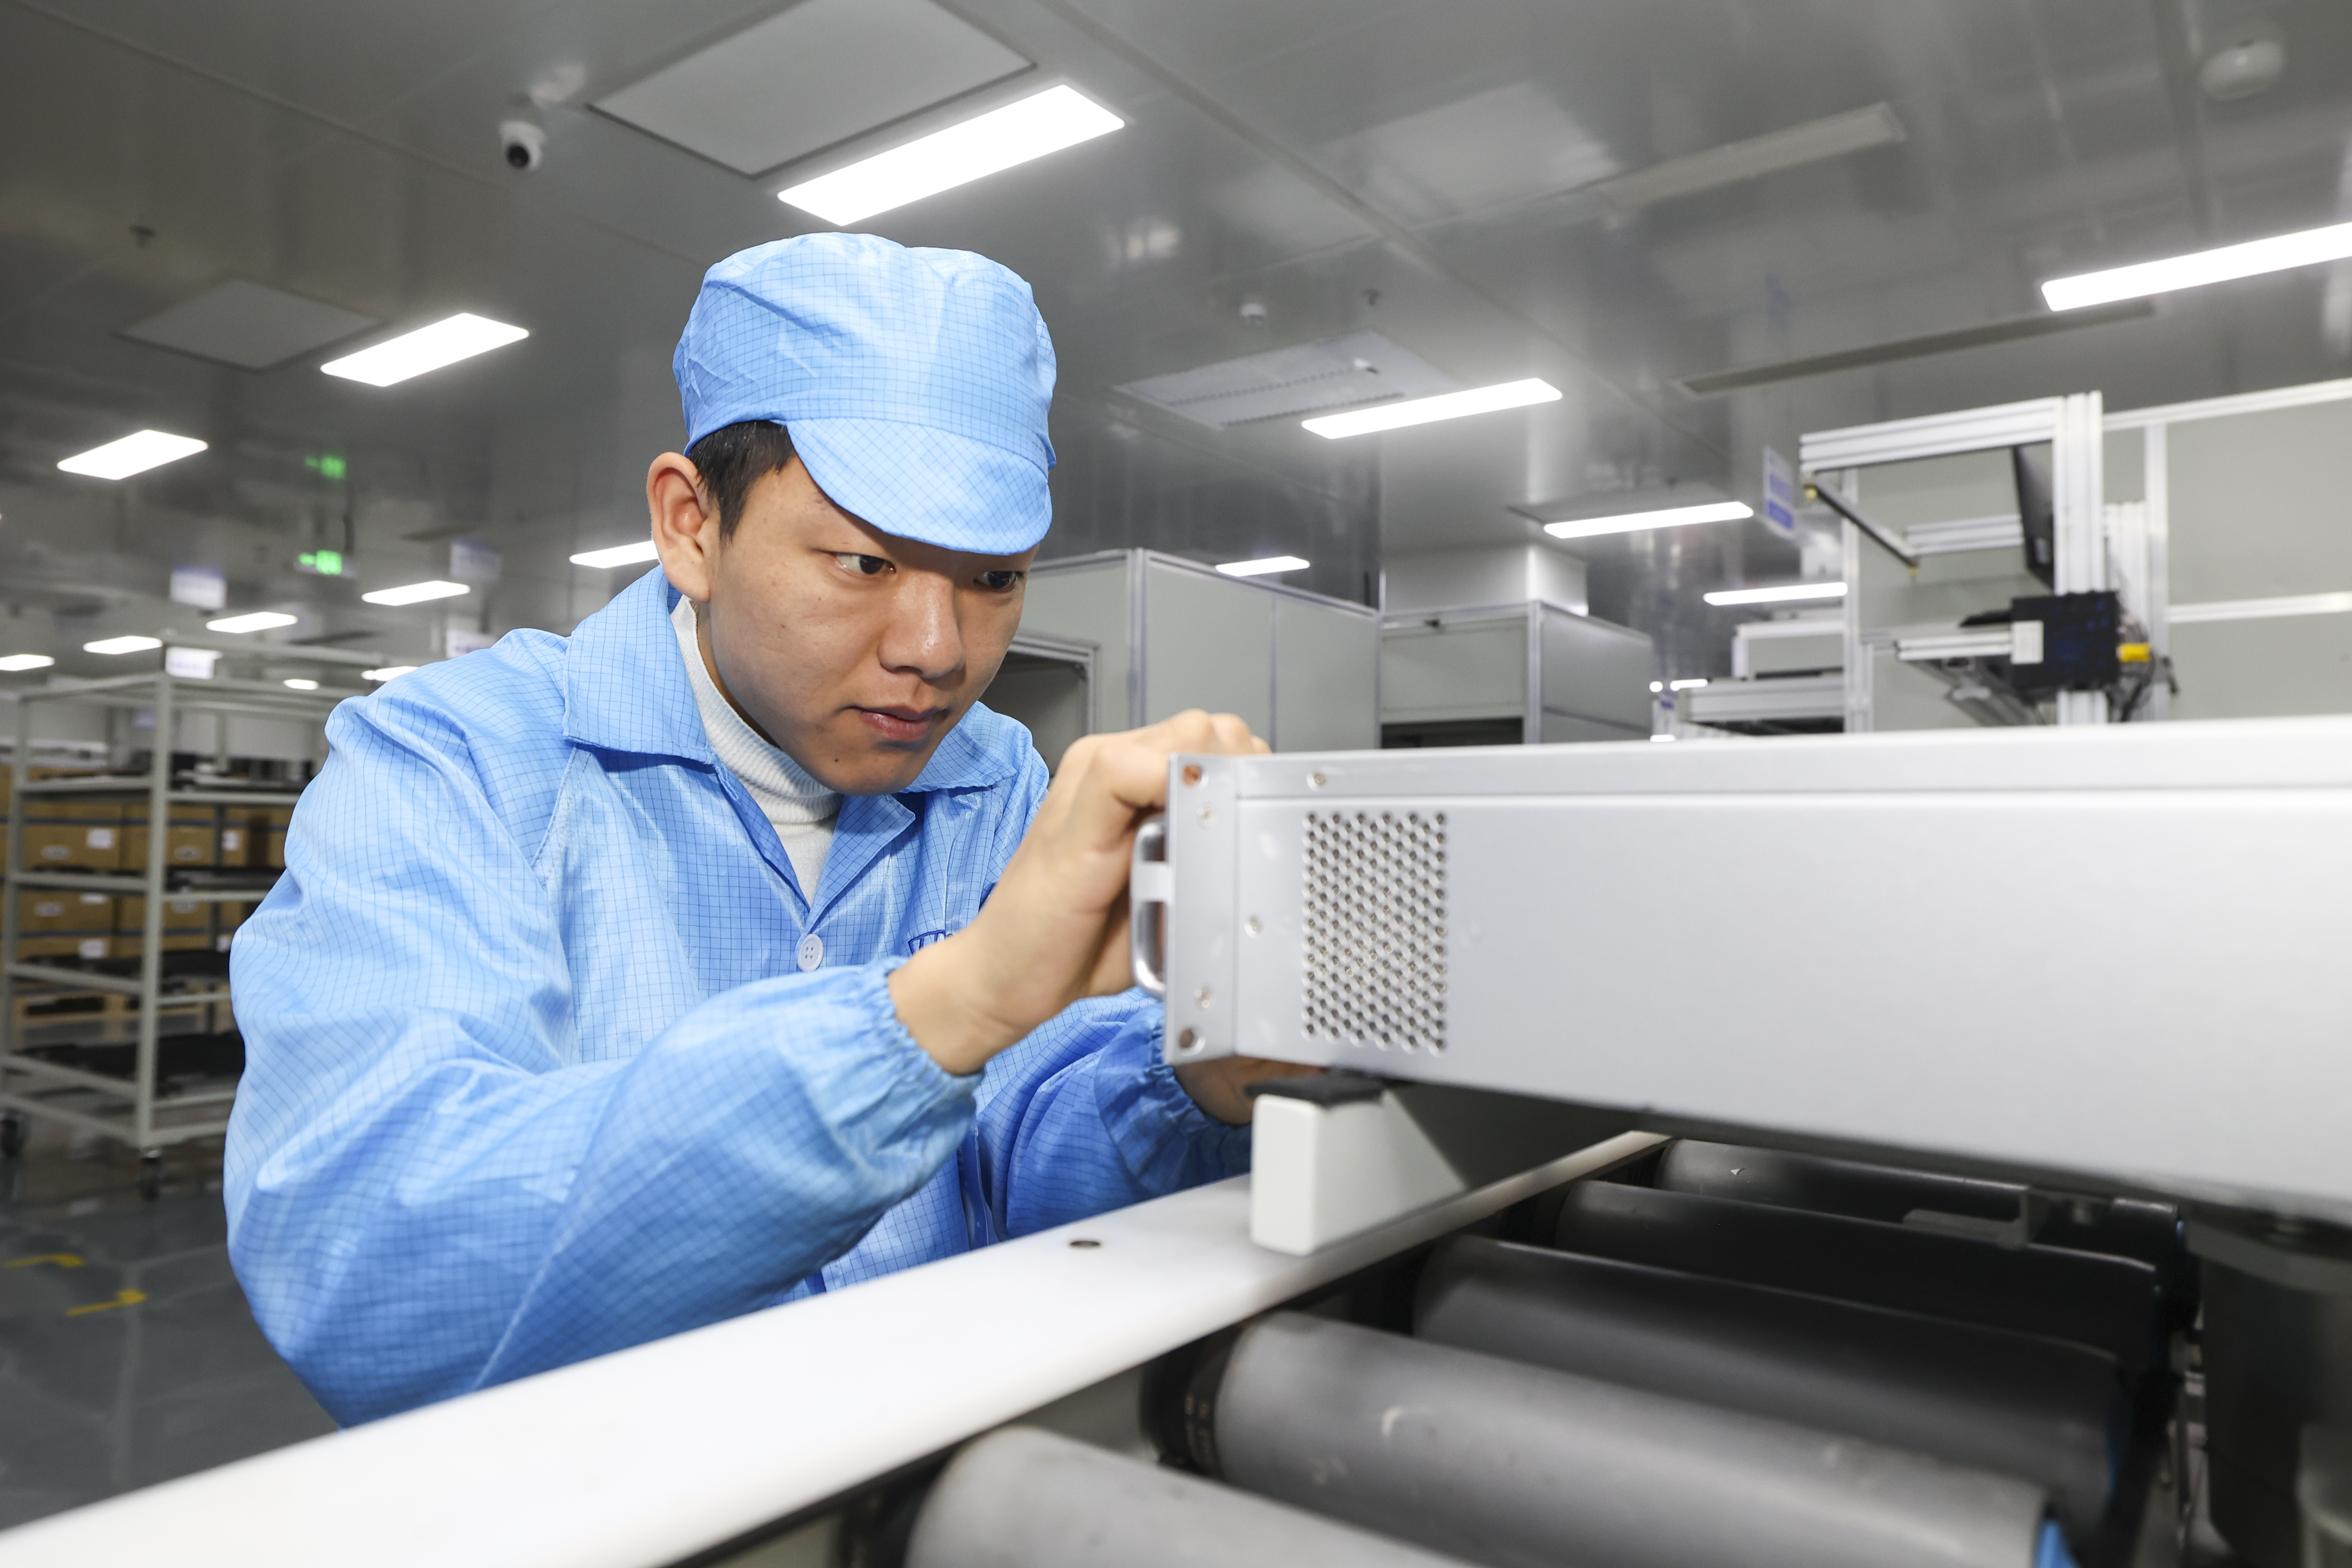
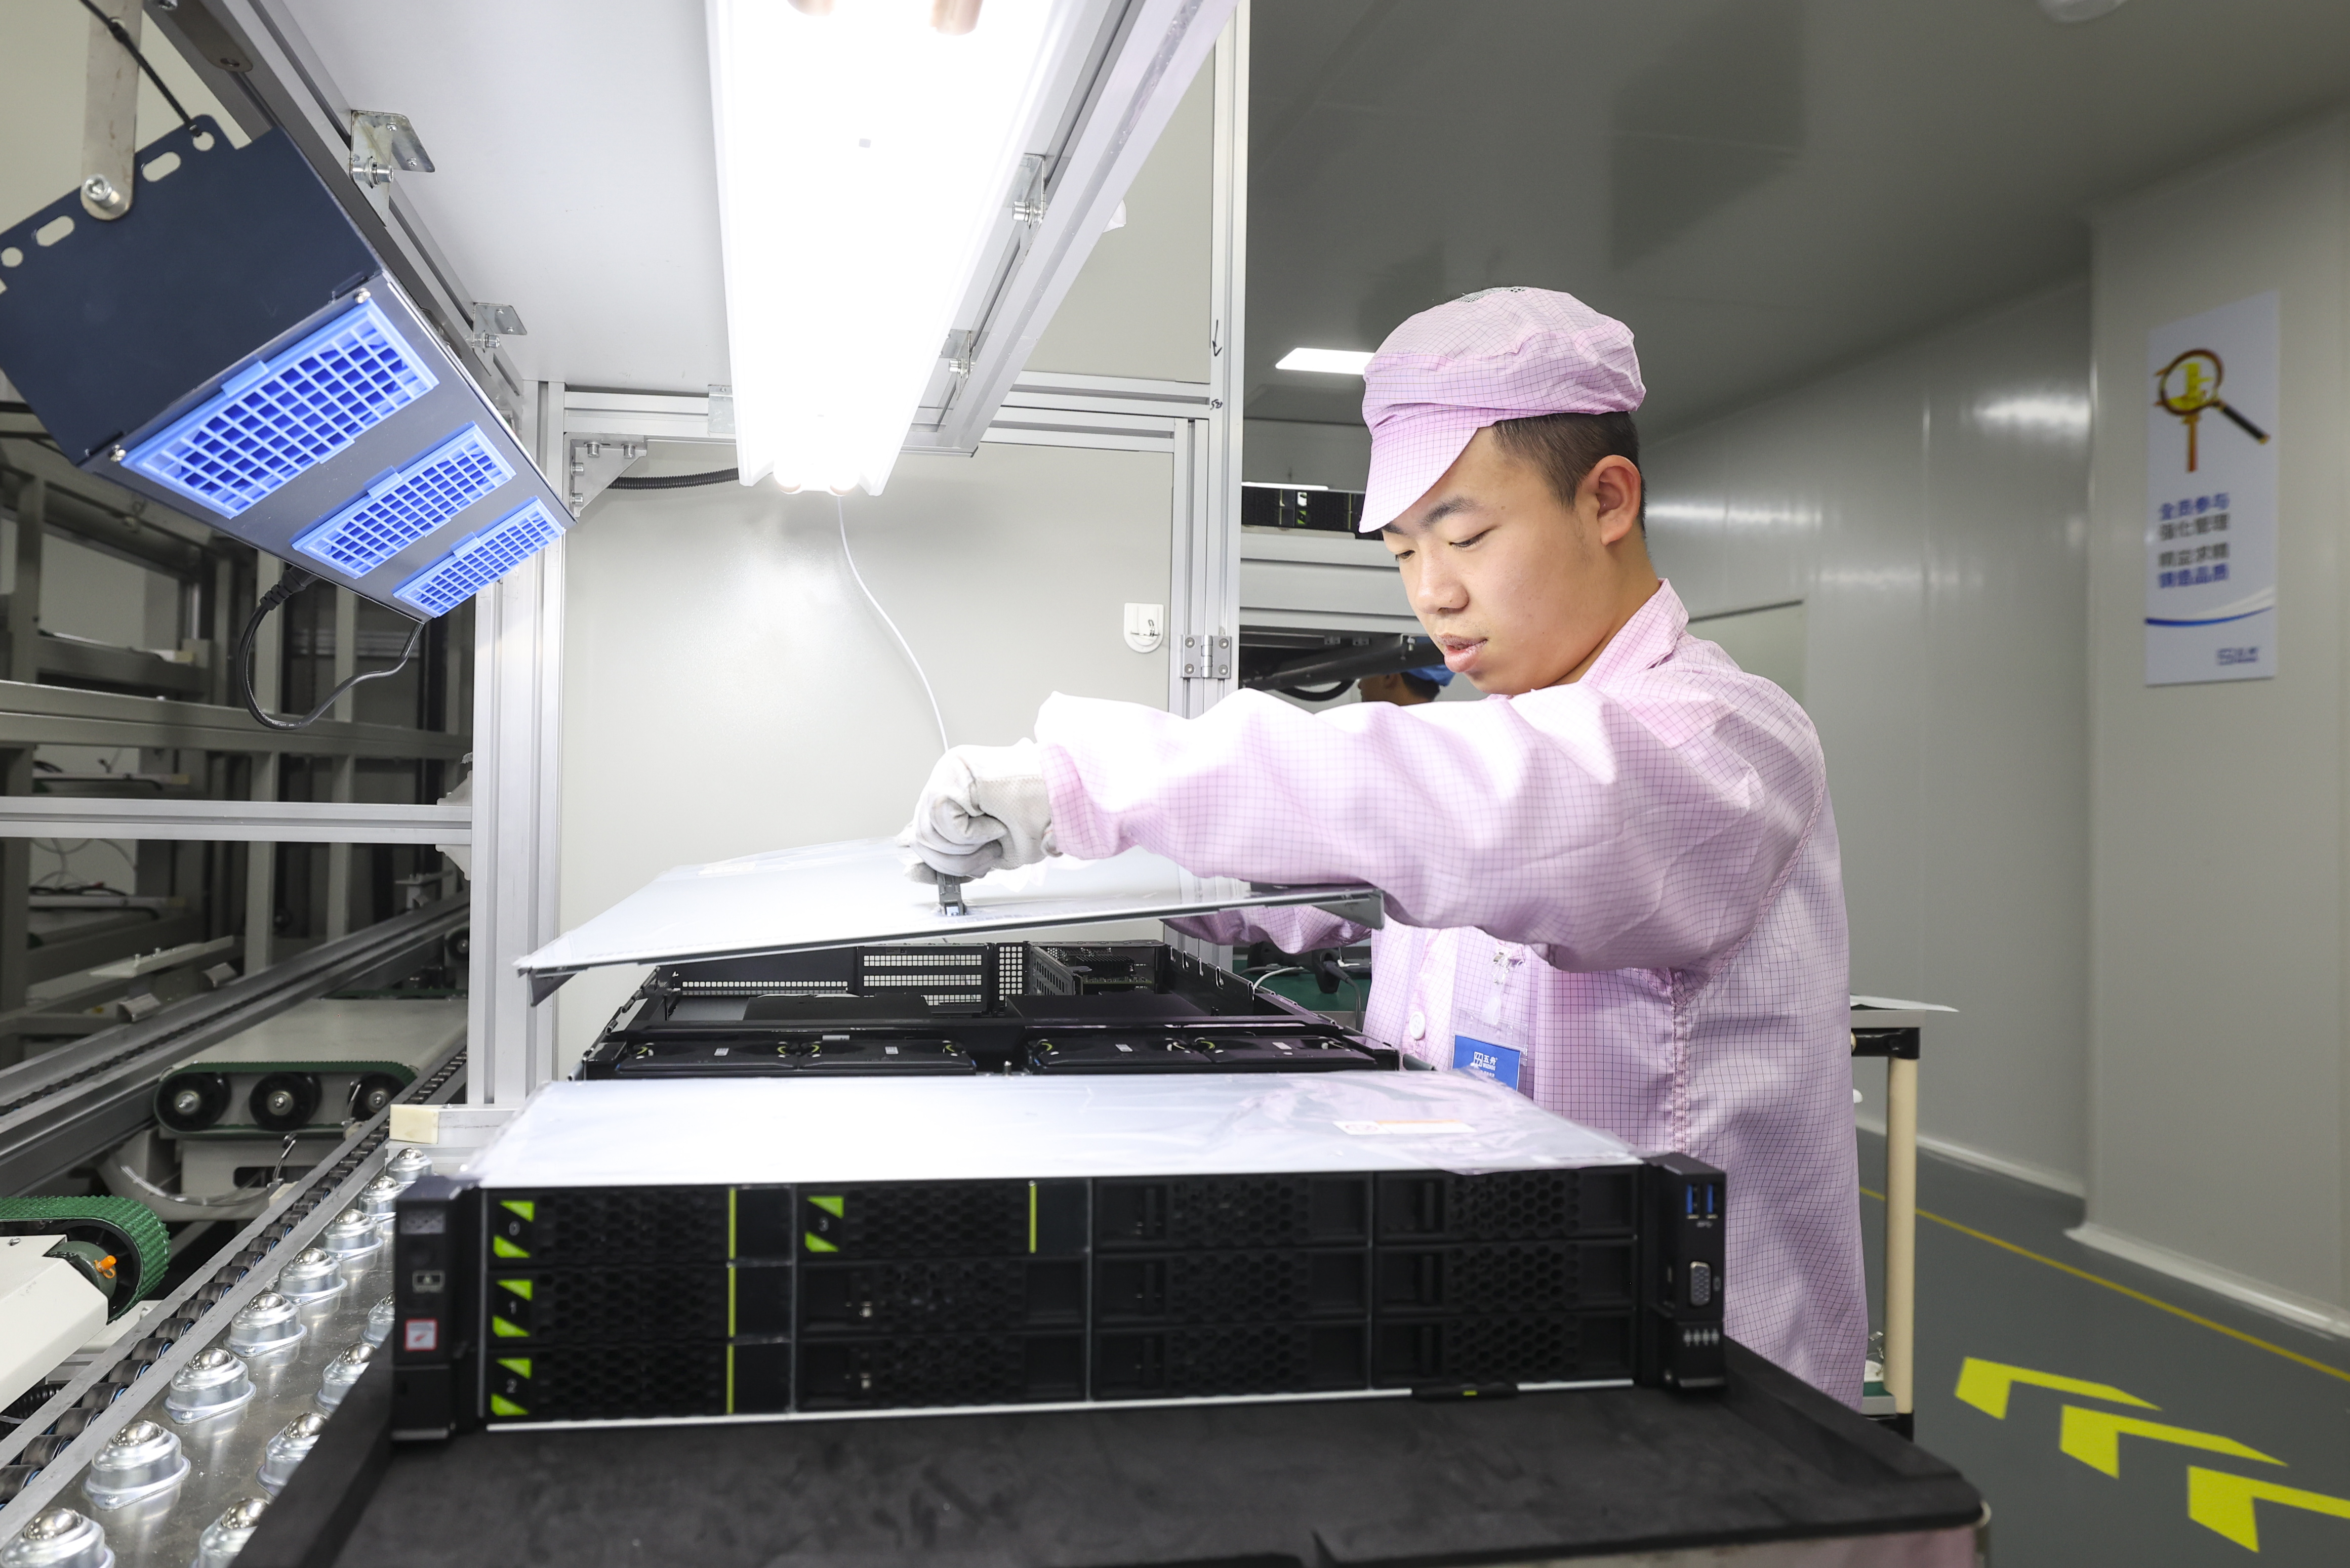
The company operates a modern manufacturing facility with a total building area of approximately 320㎡, equipped with advanced production and testing equipment to ensure strict quality control standards. CoreByte has an annual export revenue of around USD 12 million, with 6 years of export experience and over 9 years of industry experience in memory and semiconductor-related solutions.
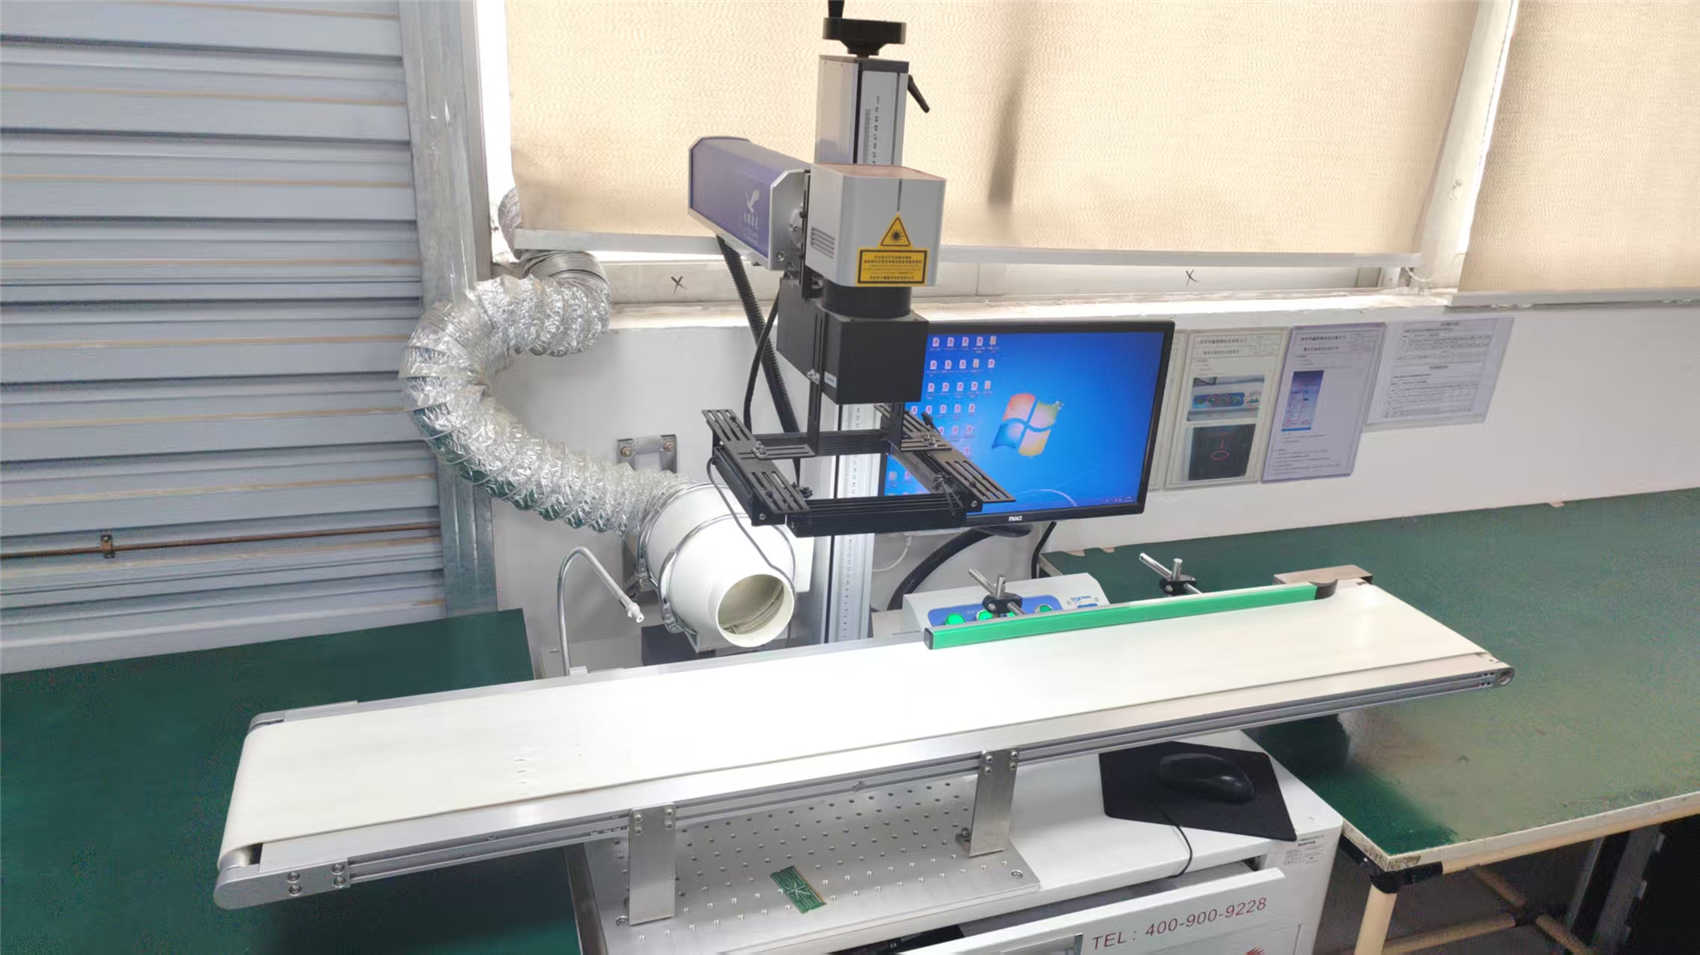
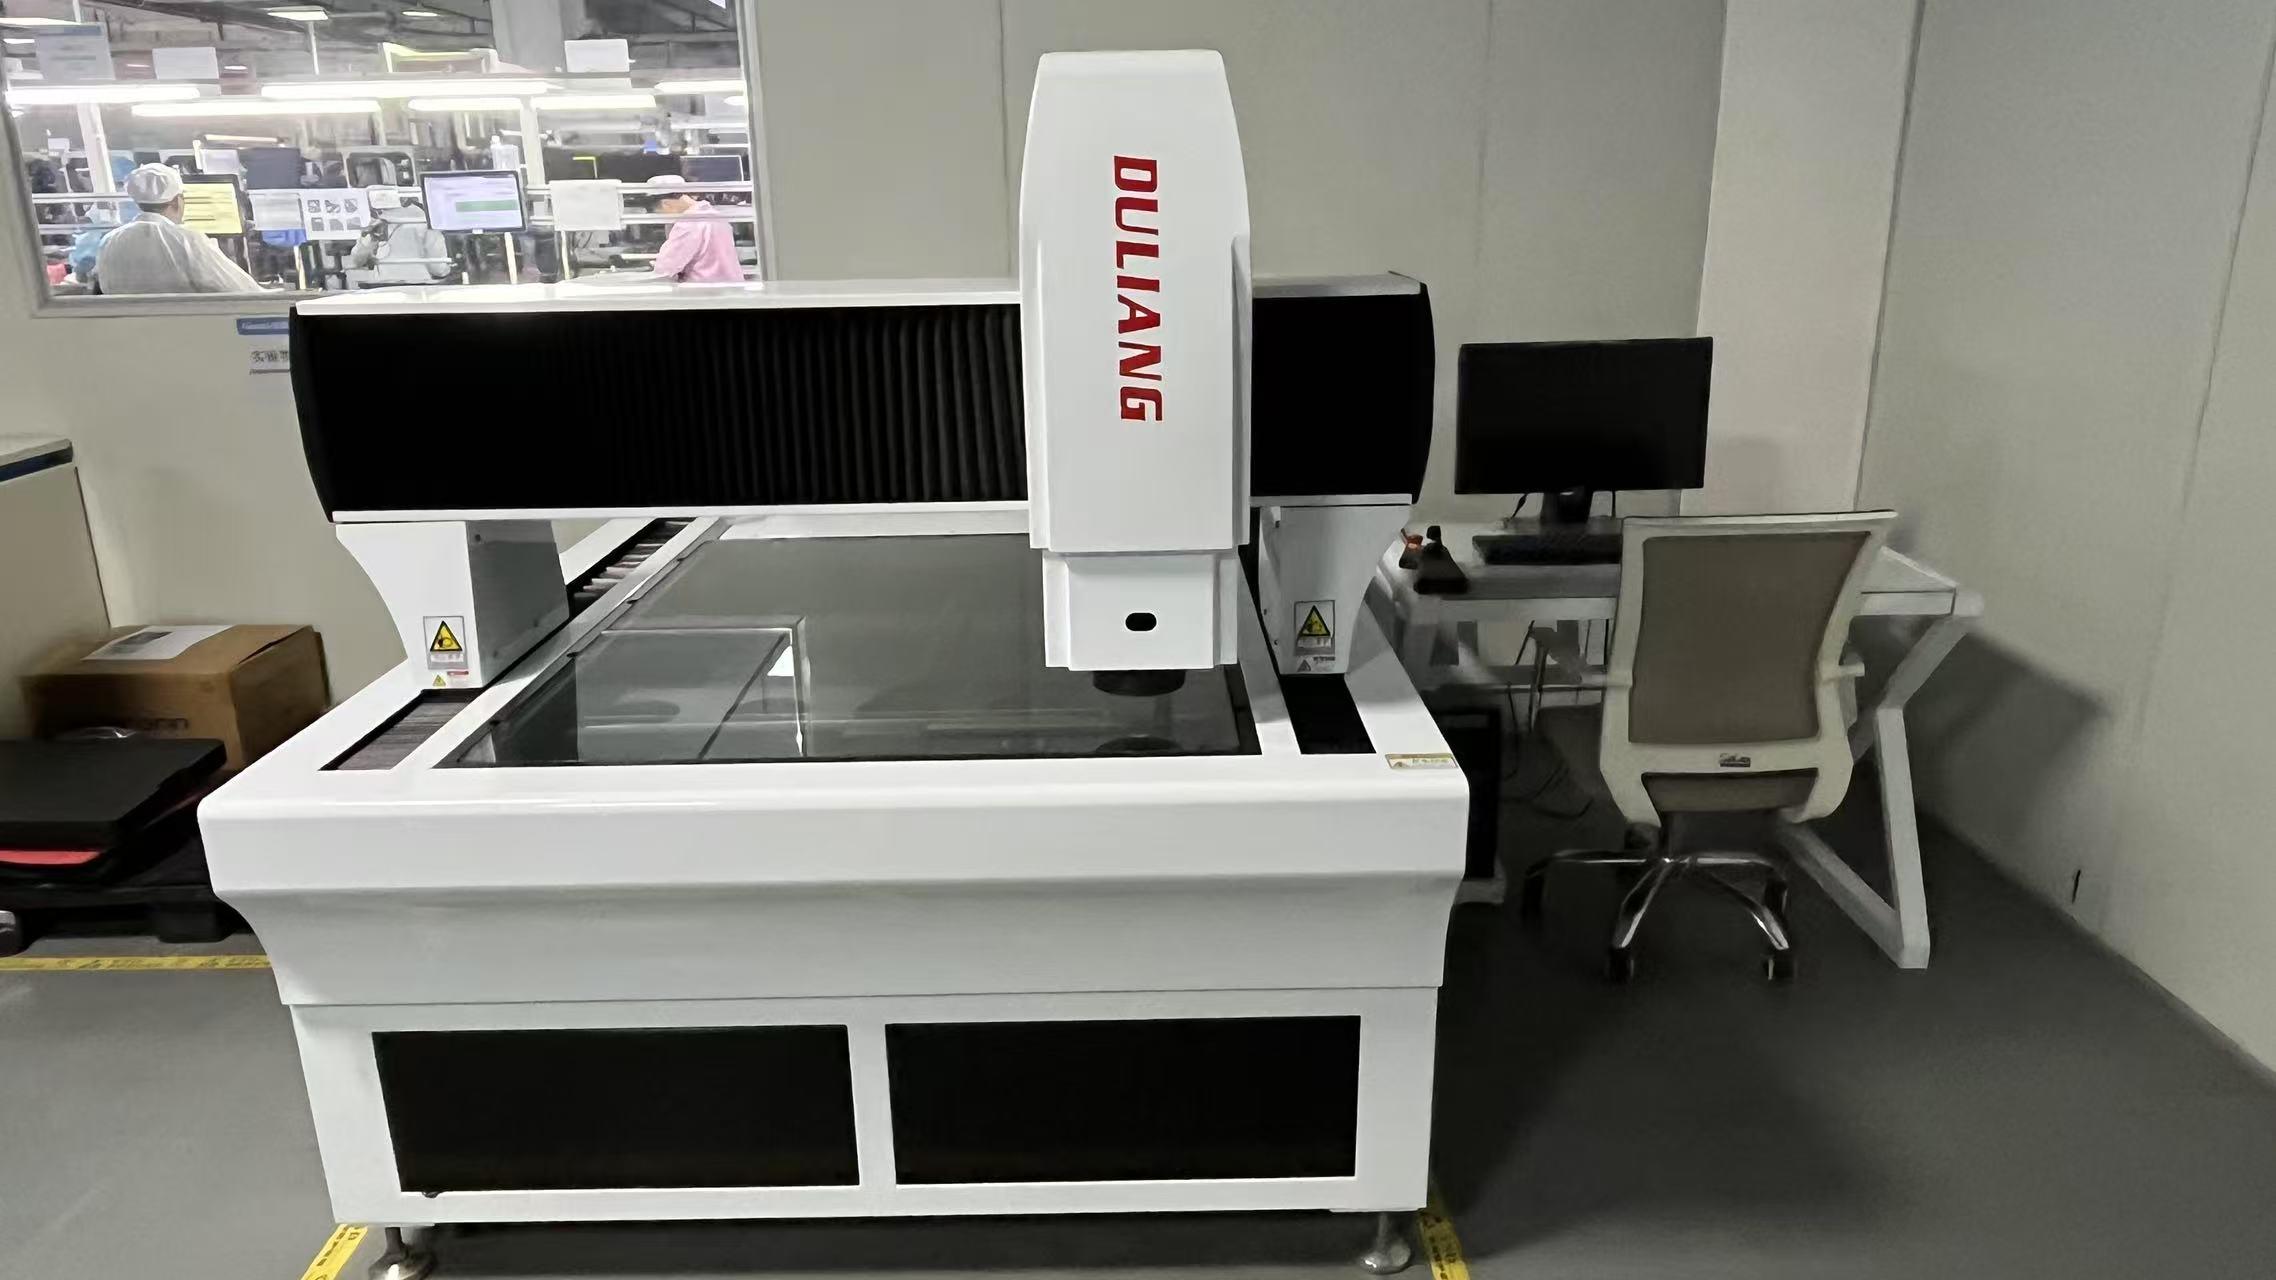
Quality assurance is a core priority at CoreByte. The company implements ISO9001-based quality management systems, combined with automated optical inspection (AOI) and high-temperature aging tests to ensure product stability and compatibility. The quality control team consists of 45 dedicated inspectors, ensuring every batch meets international performance standards.
CoreByte maintains a strong trade-oriented business background, serving key markets including North America, Europe, Southeast Asia, and the Middle East. The company has established a reliable global supply chain network with more than 1,200 supply chain partners, supporting stable production and fast delivery.
Its primary customers include OEM system integrators, server manufacturers, industrial computer brands, and data center solution providers. With strong engineering capabilities, CoreByte offers advanced customization services, including PCB design optimization, frequency tuning, thermal solution adjustment, and branding customization.
The company invests heavily in innovation, with 85 R&D engineers and launching approximately 120 new product models annually to meet evolving market demands in AI computing, cloud infrastructure, and high-performance gaming systems.
CoreByte continues to strengthen its position as a trusted global DDR5 memory supplier, committed to delivering reliable, high-speed, and cost-effective memory solutions to customers worldwide.
Navigating complex international supply chains and delivering robust technical infrastructure for modern enterprise demands.
In today's interconnected global market, enterprise buyers require robust redundancy and guaranteed component availability. CoreByte integrates tier-1 semiconductor supply networks with agile manufacturing lines, mitigating lead-time volatility and ensuring zero downtime in large-scale server deployments.
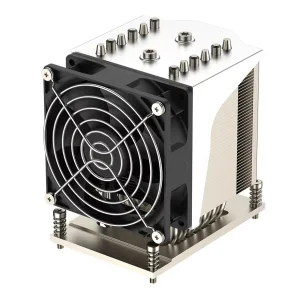
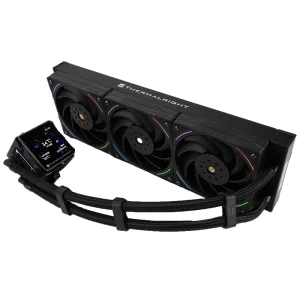
As AI workloads and high-frequency data processing push thermal thresholds higher, our advanced server cooling systems, copper-aluminum heat sinks, and precision PCBA customization provide optimal heat dissipation, ensuring peak operational efficiency under full enterprise load.
Meeting regional regulatory requirements across North America, Europe, and Asia is vital. All CoreByte products adhere to strict international compliance benchmarks, including RoHS, CE, and FCC standards, backed by local technical support and comprehensive product warranties.
Pioneering the future of high-speed data transmission, server cooling efficiency, and intelligent edge computing hardware.
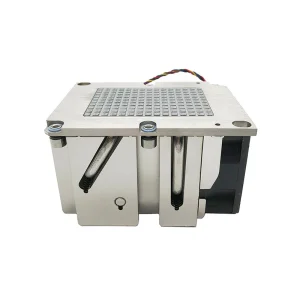
Driven by the exponential growth of artificial intelligence, machine learning, and cloud-native workloads, the hardware landscape demands unprecedented bandwidth and thermal resilience. CoreByte's engineering roadmap focuses on next-generation DDR5 memory integration, advanced server thermal management utilizing multi-heat-pipe copper configurations, and high-speed networking accessories designed to minimize packet loss and latency.
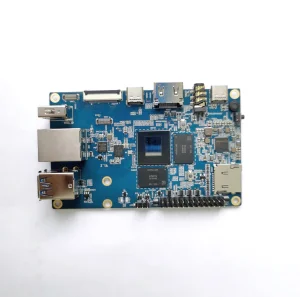
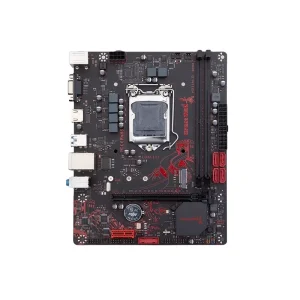
By leveraging state-of-the-art automated optical inspection (AOI) and rigorous environmental testing protocols, we bridge the gap between theoretical semiconductor capabilities and rugged, field-deployed industrial reliability. Our ongoing investments in NPU-integrated motherboards and high-frequency memory modules ensure that global system integrators stay ahead of technological curves.
Precision-engineered components built to withstand demanding industrial environments and high-intensity server racks.
Expert answers regarding our manufacturing standards, custom OEM capabilities, and global fulfillment processes.
We operate under strict ISO9001 quality management systems. Every memory module and server cooling component undergoes automated optical inspection (AOI) and high-temperature aging tests performed by our 45 dedicated inspectors.
Yes, we specialize in OEM/ODM services. Our 85 R&D engineers assist with PCB design optimization, frequency tuning, thermal solution customization, and customized heat spreader branding.
Backed by our extensive network of over 1,200 supply chain partners and advanced manufacturing equipment, standard orders are typically fulfilled and dispatched within 7 to 15 business days depending on volume.
We maintain a robust international trade network serving key enterprise markets across North America, Europe, Southeast Asia, and the Middle East with localized compliance and dedicated support.
 CoreByte